Home / Products / Aluminum Low-Pressure Casting
Main Products
Aluminum Low-Pressure Casting
Bottom-filled, low-turbulence castings for wheels, housings and safety-critical parts.
- ISO 9001 certified
- DFM feedback in 48 h
- Machined & inspected in-house
Start a New Low-Pressure Casting Quote
Upload Drawings & Get a QuoteSTEP · STP · IGES · X_T · DWG · DXF · PDF · ZIP
All uploads are secure and confidential.
Overview
Low-pressure die casting (LPDC) pushes molten aluminum up through a riser tube into the mold with 0.2–1.0 bar of air pressure. The bottom-up, non-turbulent fill gives very low porosity, excellent yield and consistent mechanical properties — the process of choice for wheels, motor housings and other round or symmetric parts.
Best suited for
- Round and symmetric parts: wheels, motor housings, end covers, bells
- Safety-critical parts that require X-ray quality
- Large thin-wall castings with high integrity
- T6 heat-treated parts with high elongation
- Medium to high volumes

Capabilities at a Glance
| Typical alloys | A356-T6, A357, 319, ZL101A |
|---|---|
| Fill pressure | 0.2 – 1.0 bar (process characteristic) |
| Typical part weight | 1 – 40 kg |
| As-cast tolerance | ISO 8062 CT6 – CT8 (typical for process) |
| Internal quality | Low porosity; X-ray inspection to ASTM E155 on request |
| Heat treatment | T6, T7 |
| Secondary | CNC machining, leak testing, painting, powder coating |
| Industries | E-motor and EV components, wheels, pump & motor housings, transmission components, rail and heavy equipment |
Tolerance and finish values are typical for the process; final values are confirmed per drawing.
Examples
Aluminum Low-Pressure Casting Parts We Produce
Motor End Cover
Ribbed dome-shaped motor cover; bottom fill keeps ribs sound and porosity-free.
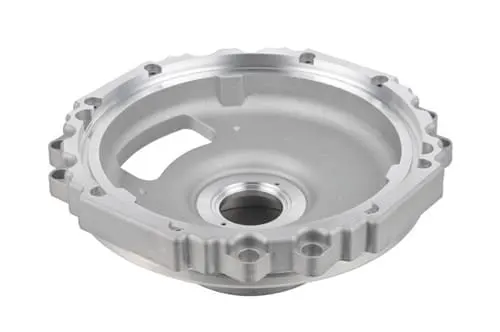
Bell Housing
Large-diameter housing with bolt flange and machined pilot bore.

Gear Case
Complex cored gear case with multiple machined bores.
FAQ
What is the difference between low-pressure and high-pressure die casting?
LPDC fills slowly from below at under 1 bar, giving dense, heat-treatable castings. HPDC injects metal at very high speed and pressure, which is faster and suited to thin walls, but parts normally cannot be T6 heat treated or welded.
Is low-pressure casting more expensive?
Tooling costs are moderate (between gravity and HPDC). Cycle times are longer than HPDC, so it is most cost-effective for parts where integrity matters.
Other capabilities
Get a quote for aluminum low-pressure casting
Send your 2D drawing or 3D model. Our engineers review every RFQ and reply with DFM feedback and pricing within 48 hours.